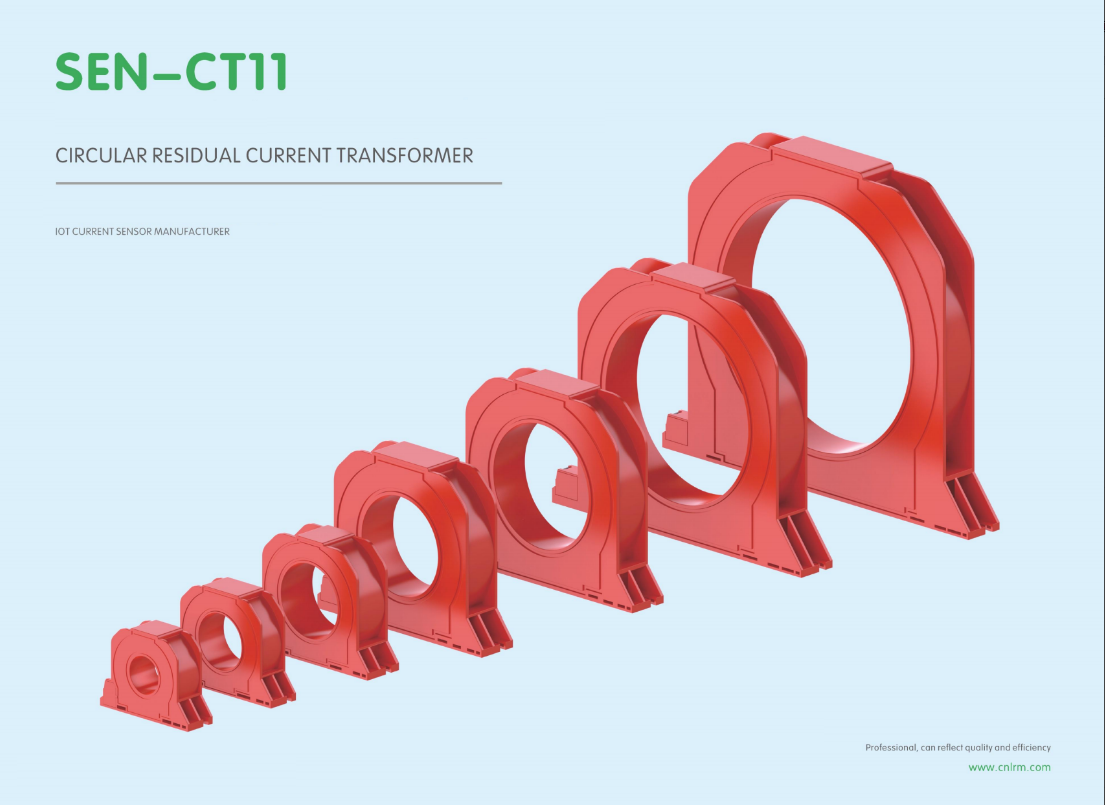
Residual Current Transformer Original Manufacturer Essential Guide for Reliable Protection
2026-08-20
When residual currents go unnoticed, the cost isn’t just downtime—it’s safety. Yet many specifiers still treat the residual current transformer as a commodity, until a nuisance trip or a missed fault forces a rethink. In this guide, we skip the generic datasheet talk and look at what separates an original manufacturer like Xiasen from resellers who can’t guarantee core performance, consistency, or long-term stability. Because reliable protection starts long before the relay sees a signal.
Why Your Residual Current Transformer Supplier Matters More Than the Datasheet
A well-written datasheet can list nominal accuracy, burden, and dielectric strength, but it cannot show how consistently those numbers hold up across production batches. Residual current transformers rely on core material quality, winding tension, and impregnation, none of which are fully captured by a specification sheet. A supplier that controls annealing, rejects cores outside a narrow tolerance band, and tests every unit under realistic residual current waveforms will give you far fewer nuisance trips and missed faults than a vendor who simply prints the same curves.
The supplier's engineering support becomes critical when your protection scheme has to handle unusual load profiles, high harmonic content, or harsh installation conditions. A knowledgeable manufacturer will ask about trip thresholds, burden loading, and even the type of relay you use before recommending a design. Datasheets rarely tell you what happens when a transformer sees a half-wave rectified residual current or how it behaves at the edge of its temperature range. The right supplier will run those tests and share the results instead of leaving you to discover the limits in the field.
Traceability and long-term support matter just as much as initial performance. If a batch starts causing false tripping or fails early, you need a supplier who can pull production records, identify the root cause, and correct the process quickly. A supplier that treats the sale as a one-time datasheet comparison will not be there when you need failure analysis or a drop-in replacement years later. Over the life of an installation, that relationship often has a bigger impact on safety and uptime than any single specification on paper.
Inside the Production Line: How Original Manufacturers Control Core Accuracy
In a high-volume machining cell, core accuracy doesn’t come from a final inspection booth. It comes from how tightly the workpiece is located before the first cut. Original manufacturers tend to rely on hydraulic or zero-point clamping systems that repeat within a few microns, while spindle preload and linear guide pre-tension are set during assembly, not adjusted in the field. These choices keep thermal growth predictable and prevent the slow drift that shows up as taper errors in a bore or runout on a shoulder.
On the floor, that control continues with in-process probing. Rather than waiting for a batch to finish, machines equipped with touch probes check critical diameters and reference faces every few cycles, then feed offsets back to the controller. The best lines push this further: they log those measurements against individual serial numbers, so a jump in tool wear shows up in the trend before it ever produces a nonconforming part.
What often gets overlooked is material consistency. Original manufacturers audit incoming castings and bar stock for hardness shifts and residual stress, because even a perfect machine cannot hold a 20-micron true position if the blank moves after roughing. Paired with strict tool-life limits and calibration intervals for the measuring equipment, these production-line controls make core accuracy a repeatable output rather than a lucky result.
The Hidden Risks of White-Label RCD Components (and How to Avoid Them)
Many distributors assume a white-label RCD is interchangeable with the branded version they’ve tested, but the internal trip coil, calibration tolerances, and even the contact materials often differ. A unit that passed a 30 mA ramp test in the lab can behave unpredictably once installed in a damp environment or paired with a specific breaker upstream. The real risk isn’t a missing logo—it’s that the manufacturer has quietly swapped a bi-metallic strip for a cheaper thermal element, shifting the trip curve enough to let a persistent leakage current go undetected until someone gets a shock.
A second hidden issue arises at the supply chain level: source tracing becomes almost impossible when you buy from a broker rather than the original OEM. If a batch of white-label RCDs develops a high failure rate six months after installation, you may have no reliable way to identify which factory actually produced the faulty boards. This lack of accountability often leads to full-site recalls that cost far more than the initial savings, not to mention the liability exposure if a fault occurs before the recall is complete.
To avoid these pitfalls, start by requesting a full tear-down report from your supplier, not just a datasheet. Ask for the actual component list, the type of residual current transformer used, and the tolerance band on the trip threshold—anything less is a red flag. Then insist on batch-level test data for every shipment, and keep a sample from each batch in your own lab for independent verification. Finally, write your purchase agreement so that the supplier must disclose any component changes with at least 90 days’ notice. If they won’t agree to that, they’re likely planning a substitution you won’t like.
Matching Residual Current Transformers to Your Protection Relay Without Guesswork
The usual mistake is picking a residual CT by ratio alone. A 100/1 or 100/5 zero-sequence CT may look fine, but if its knee-point voltage sits below what the relay demands during a heavy earth fault, the output collapses and the relay never sees the true residual current. Start with the relay's published burden and minimum sensitivity in mA or A, then work backwards: the CT's accuracy limit factor at the maximum through-fault current must be high enough to keep the secondary voltage within the linear region, accounting for the full loop resistance of the secondary wiring. This isn't a catalogue guess; it's two simple calculations: required secondary e.m.f. equals the maximum primary residual current divided by the ratio, times the total secondary circuit impedance. Compare that against the CT's magnetising curve, not just the nameplate VA rating.
A second common trap is undersizing the CT window or ignoring the influence of cable capacitance and asymmetrical currents. If three phases plus neutral pass through the window, the CT's residual output is zero only when the cable geometry is perfectly symmetric and there is no standing leakage—conditions that rarely hold on long feeders. For relays with adjustable residual pickup down to 10 mA or less, you need a CT with a low secondary leakage reactance and a core material that does not remanence easily. Rather than relying on published typical curves, request the actual excitation curve from the manufacturer and verify it against the relay's minimum operating point. When the relay has a built-in CT supervision or a settable burden, use that value, not an assumed 0.5 VA. This removes the guesswork because the match is based on measured data, not on 'experience.'
Custom Core Design: When Standard Ratios Are Not Enough
Off-the-shelf cores force you to accept a fixed relationship between window area, cross-sectional area, and mean turn length. Once you push switching frequency higher or shrink the board footprint, those standard proportions start working against you—windings get cramped, copper losses climb, and thermal bottlenecks appear where you can least afford them. Custom core geometry lets you rebalance those trade-offs instead of fighting them.
A well-chosen custom shape does more than squeeze out a few extra watts. It can align the flux path with the winding layout, reduce leakage inductance in resonant topologies, or open up a dedicated cooling channel through the center leg. Rather than adapting your circuit to an off-the-shelf part, you specify the core around the actual current density, duty cycle, and isolation requirements—then let the magnetics fit the design, not the other way around.
Field-Proven Reliability Checks That Separate Real Manufacturers from Resellers
A genuine manufacturer distinguishes itself long before a purchase order is signed, and the difference becomes undeniable once you step onto the production floor. Resellers can show you polished brochures and third-party spec sheets, but they rarely open the door to live assembly lines, raw material storage, or in-house testing rigs. Field-proven reliability checks—those carried out on actual hardware under real working conditions—demand a level of transparency that only a company with its own engineering and fabrication capabilities can offer. If a supplier hesitates to let you witness a stress test or inspect a batch mid-production, you are likely dealing with a middleman who has never touched a torque wrench.
The most telling verification happens when you ask to see how products are validated before shipping. Real manufacturers run cyclic load tests, environmental chamber trials, and destructive sample analysis on a routine basis, and they keep detailed logs that trace every component back to its heat lot. These checks are not marketing theatre; they are built into the workflow because the company's reputation rests on repeat orders from industries that cannot tolerate field failures. In contrast, a reseller can only repeat what an overseas factory told them, often without ever visiting that facility. The absence of first-hand test data, calibration certificates for their own equipment, or a dedicated quality engineering team is a red flag that no amount of glossy documentation can cover.
Practical field checks include prolonged soak tests under rated load, tear-down inspections of randomly pulled units, and verification of welding or casting integrity using non-destructive methods. A real manufacturer will welcome these requests and often has a customer viewing area near the test lab. They might even hand you a sample that has just come off the durability rig, still warm from cycling. A reseller, by contrast, will deflect with promises of factory audits that never materialize or offer only a pre-selected 'golden sample' that was never representative of production output. Over time, these field-proven checks create a paper trail of performance that separates the companies accountable for their hardware from those merely shuffling containers.
FAQ
Focus on core material quality, winding precision, and insulation testing. Check if the manufacturer provides detailed magnetization curves and thermal ratings, not just generic datasheets. Field failure rates and customization capability also matter more than marketing claims.
Original manufacturers control the entire production chain, from core annealing to encapsulation, which reduces variability. That consistency means the transformer trips predictably under low fault currents, preventing nuisance tripping or failure to operate when it counts.
Many buyers assume a simple ratio check is enough. A genuine manufacturer performs impulse voltage tests, temperature cycling, and linearity verification across the full residual current range. This catches partial winding shorts or core saturation that only appear under stress.
Yes, if the manufacturer understands the relay's burden and frequency response. Proper customization matches the core cross-section to the relay input impedance, maintaining accuracy at low residual currents instead of forcing a generic transformer into an incompatible circuit.
Common hidden issues include moisture ingress at lead exit points, micro-cracks in resin encapsulation, and poor shield grounding. Original manufacturers use vacuum potting and partial discharge testing to eliminate these weak spots before shipping.
High harmonic environments, wide temperature swings, or vibration require different core materials and potting compounds. A reliable manufacturer asks about the actual installation location first, then recommends a transformer that won't drift or crack under those conditions.
Beyond a calibration certificate, request accelerated aging test reports, failure mode analysis for the specific design, and a traceability record linking each unit to its raw material batch and test data. If they hesitate, treat that as a warning sign.
Conclusion
The choice of residual current transformer manufacturer shapes protection outcomes long before any datasheet reaches your desk. A supplier that controls winding tension, core annealing, and magnetic shielding on its own floor can hold ratio error and phase shift under varying burden and temperature. That is what separates original production from white-label sourcing. When you buy through a reseller, you inherit undocumented substitutions in core material or potting compound, and those changes may not appear in a standard accuracy curve yet can mislead a sensitive relay. The real question is not whether a printed spec meets IEC 61869-2 or similar, but whether every batch meets it after thermal cycling and vibration.
Matching the transformer to the relay requires more than picking the same rated residual current. You need to know the relay's minimum operating burden, its input impedance, and how it behaves at the knee of the core's excitation curve. In many retrofit or harmonic-heavy installations, a standard 30 mA or 300 mA ratio is too blunt. Custom core design—adjusting lamination grade, secondary turns, and shielding—lets the transformer deliver a clean secondary signal at the relay's actual threshold without nuisance tripping or saturation. Field-proven checks matter here: measuring composite error under a known residual current, verifying immunity to adjacent phase conductors, and confirming long-term stability after moisture exposure. Real original manufacturers will invite these tests or provide the data from their own; resellers usually cannot. That evidence, not the logo or the catalog copy, tells you whether the protection will hold when leakage current rises on a wet installation or after a motor winding degrades.
Contact Us
Contact Person: Liu Mengyang
Email: [email protected]
Tel/WhatsApp: 8618727589233
Website: https://www.cnlrm.com/en/