Custom Bolts Manufacturer That Delivers Precision and Durability
2026-09-27
When a standard bolt fails, the cost isn't just downtime—it's trust. That's why custom bolts demand more than off-the-shelf precision. At Peak Fasten, we engineer every fastener to deliver both the precision your assembly requires and the durability your reputation depends on.
Machined to the Numbers You Actually Need
It’s easy to get lost in spec sheets full of theoretical limits and peak outputs that never show up in real work. What we focus on instead is the actual performance envelope you’ll experience day to day. Every dimension, tolerance, and surface finish is measured against the loads, speeds, and cycles your operation really sees — not some idealized lab scenario. That means when we say a part is machined to a certain number, it’s a number that holds up under your tooling, your feed rates, and your shop floor conditions.
Instead of chasing arbitrary precision on every surface, we dial in the critical features where tight control actually prevents failure or extends tool life. The rest gets a sensible, economical finish that keeps your costs predictable. This targeted approach comes from years of collaborating with machinists and production engineers who told us the same thing: give me the numbers that matter for my setup, not a glossy brochure figure.
What you get is a component that fits your process like it was measured on your own CMM. No guesswork, no excessive over-engineering, and no hidden rework because a tolerance stack-up went sideways in the real world. Just honest machining that respects both your blueprint and your bottom line.
Small Batches, Serious Standards
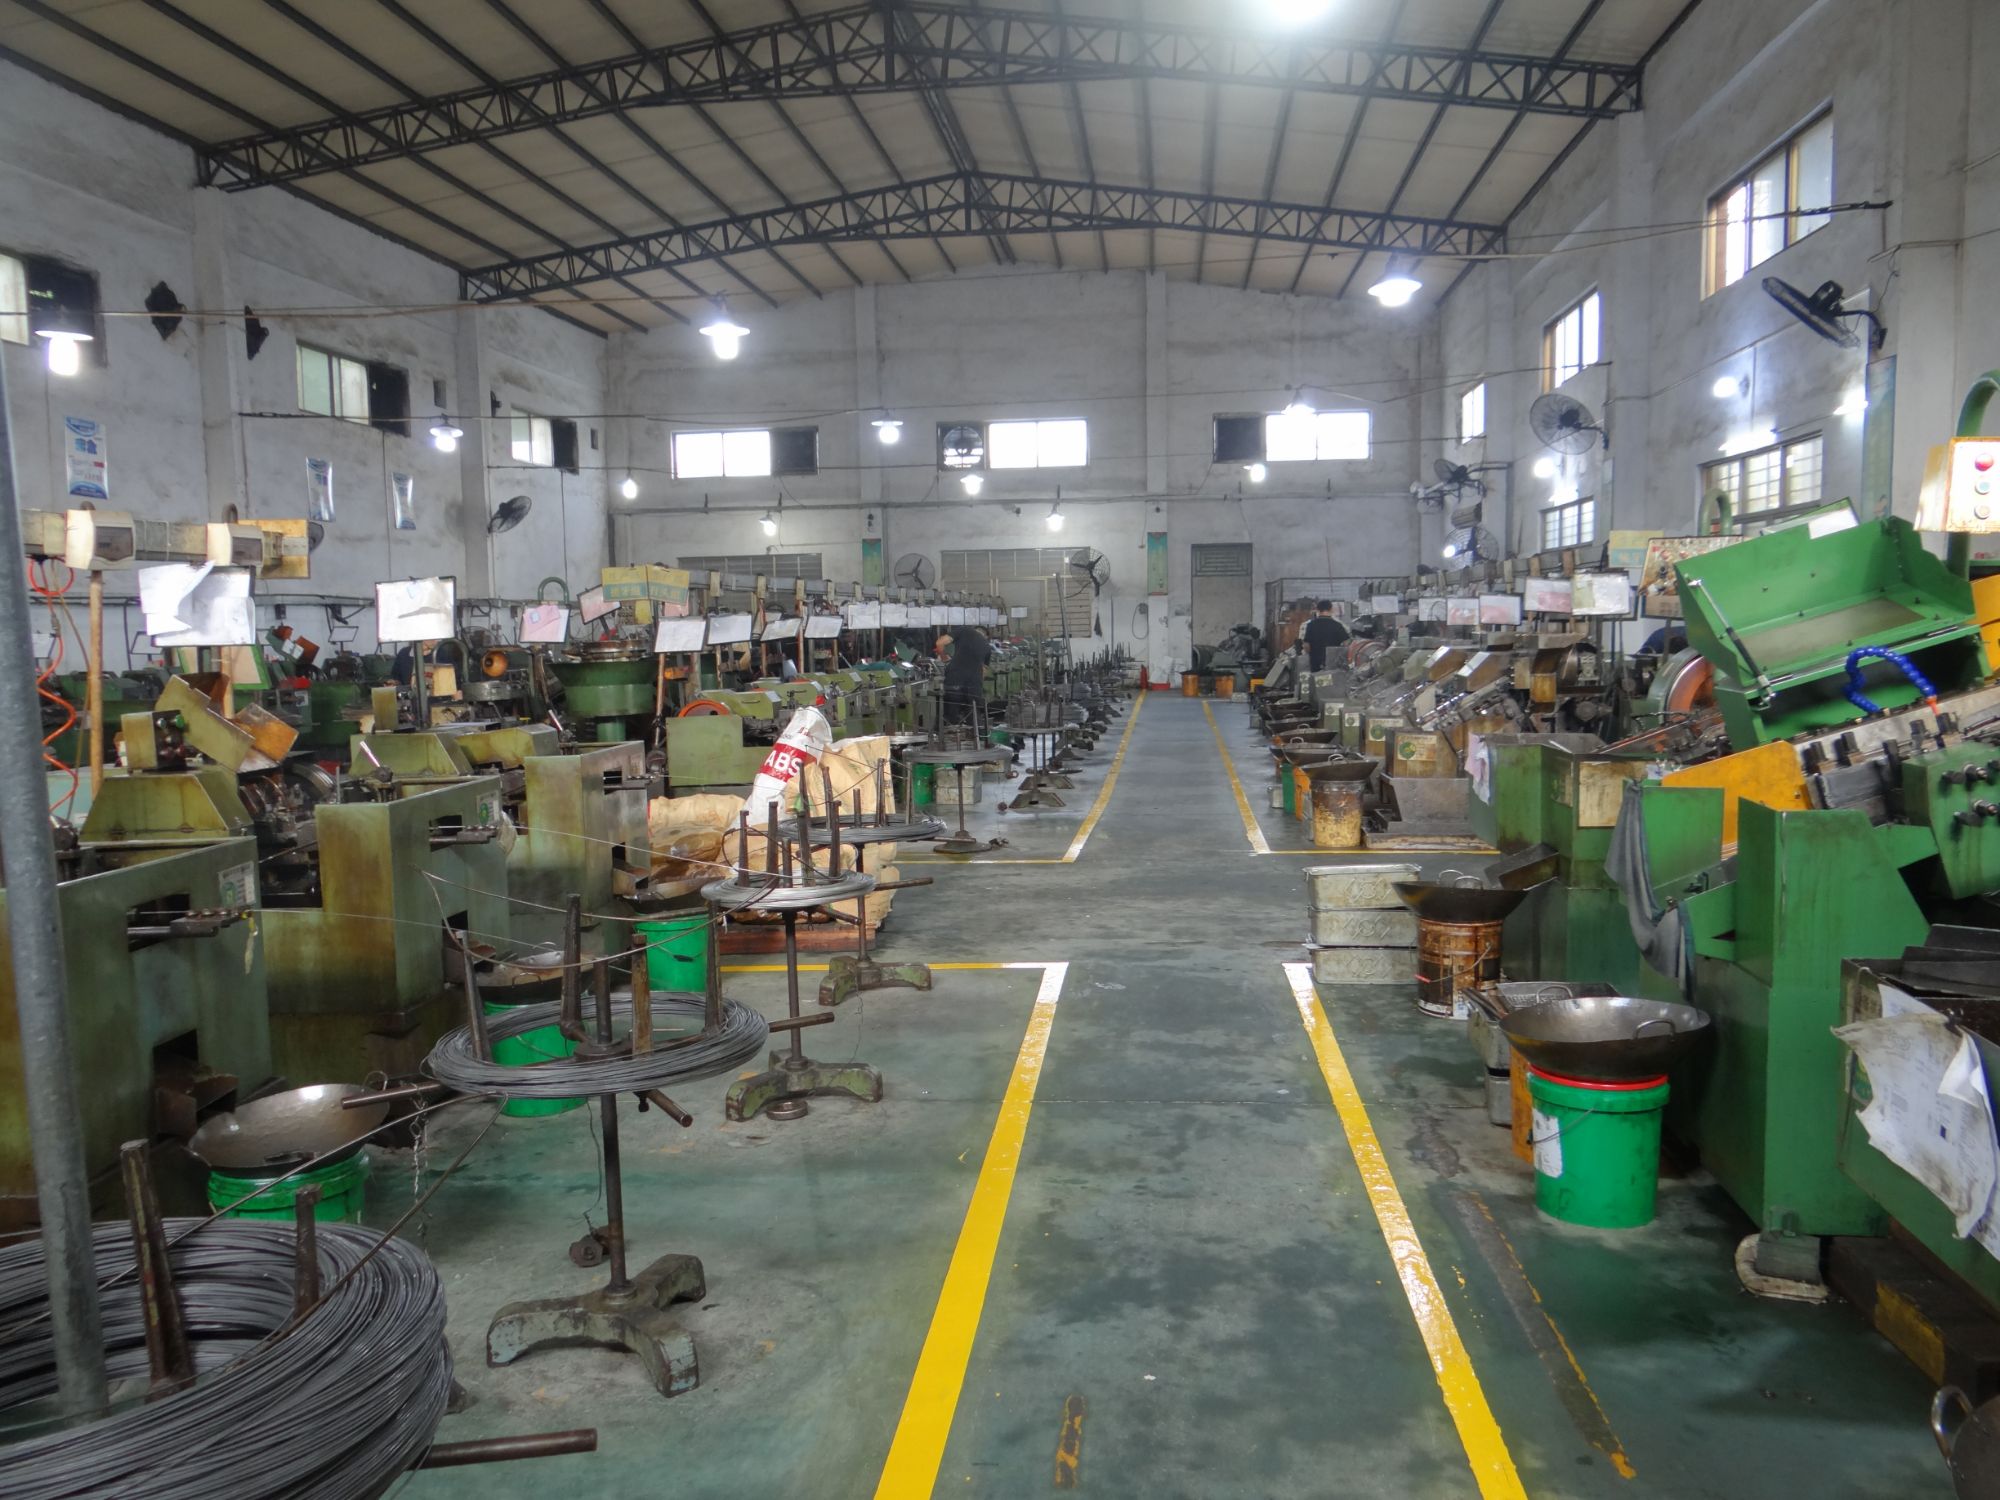
We don’t chase volume. We chase the moment a batch comes together exactly right—color, texture, scent all landing where they should. Working in small quantities lets us adjust by feel, not by spreadsheet, so every run gets our full attention from first measure to final check.
That means if a raw material doesn’t meet the bar, we pause. If the temperature drifts a few degrees, we start over. There’s no assembly line to hide behind, and honestly, we like it that way. The standards are set by people who actually use what we make, not by a checklist written for someone else’s factory.
It’s slower, sure. It costs more. But the result is something we’d happily put our own name on every single time—and if we wouldn’t, it doesn’t ship.
Materials That Don't Flinch at Stress
Most structural materials fail long before their theoretical strength because tiny flaws grow into cracks under repeated loading. The exceptions are those engineered to shrug off stress concentrations: twinning-induced plasticity steels absorb energy by rearranging their crystal lattice on the fly, while certain ceramic-matrix composites use distributed microcracking to prevent any single crack from becoming dominant. These are not simply stronger in a tensile test—they remain stable after thousands of cycles that would embrittle conventional alloys.
A closer look at stress-tolerant materials often reveals deliberate architectural tricks rather than one magic formula. High-entropy alloys mix five or more principal elements to create severely distorted lattices that hinder dislocation motion without sacrificing ductility. Nature offers another route: nacre, the iridescent lining of abalone shells, combines brittle aragonite platelets with a tiny fraction of biopolymer, yielding a toughness far beyond either component alone. Engineers have copied that layered strategy in metal-ceramic laminates that blunt cracks by forcing them to follow tortuous paths.
Real-world deployment pushes these materials into environments where failure is not an option: gas turbine blades spinning at 10,000 rpm under thermal gradients, or deep-sea connectors subjected to cyclic pressure at 6,000 meters. The best candidates do not just survive a single dramatic overload; they accumulate negligible damage over decades, often thanks to self-healing mechanisms or phase transformations that close nascent cracks. That is the real meaning of not flinching—not a one-time display of toughness, but a quiet refusal to degrade when stress becomes routine.
Your Specs, Not a Catalog Compromise
Most catalogs force you to bend your project around whatever happens to be on the page. That might mean settling for a length that is almost right, a material that is close enough, or a finish that looks fine but not exactly what you had in mind. None of that belongs in a space you have already designed down to the last detail. We start from your measurements, your material choices, and your tolerance for the smallest edge radius. Nothing gets swapped for a stock alternative unless you explicitly ask for it.
You do not have to redraw your plans to fit a predefined size range. Send over the exact requirements, from overall dimensions to hole placements, surface texture, and even packaging constraints. Our production team treats those numbers as the starting point, not as a wish list. The result is a component that matches your drawing instead of a catalog item that forces you to change the drawing.
The difference shows up in the final assembly. There are no awkward shims, no visible gaps, no last-minute calls to "make it work." What you receive is built to the specification you supplied, which means your design keeps its original intent without compromise. It is a simpler way to work, especially when the person approving the build is also the person who wrote the specs.
Threads That Hold When It Counts
There’s a quiet kind of strength in the things that don’t snap under pressure—the worn stitching on a climbing rope, the reinforced seam of a sail mid-storm, the familiar rhythm of a teammate’s voice when the plan goes sideways. These are the threads that hold when it counts, and they rarely advertise themselves. They earn trust slowly, through repetition and repair, until one day you realize you’ve stopped checking for frayed edges because they’ve never let you down.
In moments that test everything, it’s rarely the newest gear or the loudest confidence that carries you through. It’s the old, mended, unglamorous layer of preparation—the knot you’ve tied a thousand times, the backup generator that hums on, the quiet commitment that doesn’t need an audience. Those threads aren’t flashy, but they’re the reason you’re still standing when the dust settles.
So ask yourself: what are you relying on when the margin for error disappears? Build those threads now, not in the crisis. Because when the load comes—and it always does—you’ll want something that holds not because it’s perfect, but because it’s true.
From Prototype to Production Without the Runaround
Moving from a working prototype to a full production run often feels like navigating a maze designed by someone who's never actually built anything. The usual path is littered with endless revision loops, surprise tooling costs, and manufacturers who vanish when you need a small design tweak. It doesn't have to be that way. By working with a partner who understands both the creative mess of prototyping and the discipline of production, you can skip the frustrating detours. Your design stays intact, your timeline shrinks, and you don't have to re-explain every detail to a new vendor.
The trick is finding a team that treats your prototype as a conversation, not a final answer. Early-stage flaws get caught before they become expensive molds or circuit boards. Materials are tested in small batches, not guessed at. Then, when it's time to scale, the same people who helped you iterate are the ones running the line. No handoff documents, no lost nuance, no 'that's not how we do it here.' Just a clean transition where the product you approved is the product that ships.
If you're tired of the runaround, look for a process that values transparency and technical honesty. You want someone who will tell you when a snap-fit needs more ribbing or a finish will scuff in transit — before you've committed to 10,000 units. That kind of straight talk keeps your project moving, your costs predictable, and your sanity intact. Because going from prototype to production shouldn't feel like a punishment; it should feel like the natural next step.
FAQ
We design around your actual load, environment, and mating parts instead of making you adapt to a catalog size. Thread fit is checked on calibrated gauges, and every dimension is held to your print.
Alloy steel, stainless, titanium, and nickel alloys are all on the table. If corrosion or galling is a problem, we can apply zinc-nickel, PTFE, or ceramic coatings.
We use live-tooling lathes and multi-axis mills with in-process probing. Critical features get a final CMM pass, and inspection records are kept for each batch.
Send us the part that failed or wore out. We'll measure it, create a model, and reproduce it, often with a material or geometry upgrade if you'd like.
Heavy equipment, energy, marine, aerospace, and industrial automation. A lot of our work comes from maintenance teams chasing a failure or engineers building a new assembly.
Simple turned parts usually ship in 2–3 weeks. More complex bolts with heat treatment and plating can take 4–6 weeks. Once we see the drawing, we'll give you a firm date.
We can include material certs, heat lot traceability, dimensional reports, and test results like tensile, hardness, or salt spray. We'll match the paperwork to your quality team's needs.
Yes, we routinely run 10–50 piece prototypes, make fit or torque adjustments, and then scale up without changing the process.
Conclusion
Every custom bolt we machine starts with your actual numbers, not a rounded-off guess. Whether you need a shoulder diameter held to a few tenths or a thread pitch that barely deviates from the print, the part comes off the lathe exactly as drawn. That matters because off-the-shelf hardware always forces a compromise somewhere—a slightly longer grip, a softer corner, a coating that fights the torque spec. Our shop runs small batches, so each order gets inspected like a prototype, not sampled like a production run of ten thousand. The materials we pull from the rack—4140, 17-4PH, Inconel, titanium—don't flex or gall when the load spikes, and heat treating is dialed in per lot, not per catalog number.
If your assembly has a bolt that nobody stocks, we don't ask you to redesign around a standard part. Send the spec, even a rough sketch, and we cut the threads, undercuts, and drive features your way. When those threads have to hold through vibration, thermal cycling, or a safety-critical joint, the fit is checked with go/no-go gages and verified under load, not just eyeballed. From the first prototype to a repeat order of two hundred, the process stays the same: your drawing drives the machine, the inspection report comes back with every dimension, and the parts ship without a round of emails about substitutions. That's what precision and durability actually look like—no catalog compromise, no runaround.
Contact Us
Contact Person: Mason Lv
Email: [email protected]
Tel/WhatsApp: +86 13027998452
Website: https://www.peakfastentech.com